
Counting and Bottling Accuracy in Pressed Candy OEM: Lines, Checks, Rejects
The last packaging step before a tablet leaves the factory is counting the cores into a bottle or a blister. For pressed candy the cores are light and the count per bottle is high, so small counting errors get amplified. Underfill by a few tablets and consumers complain; overfill and you give away raw material and packaging batch after batch. Many brand owners focus on tablet weight control at the press and overlook the filling line, even though counting accuracy is just as measurable and just as contractible. In pressed candy OEM, counting and bottling is usually managed as its own process unit, with its own principles, its own error sources and its own acceptance method. This article goes through the critical points in production order.
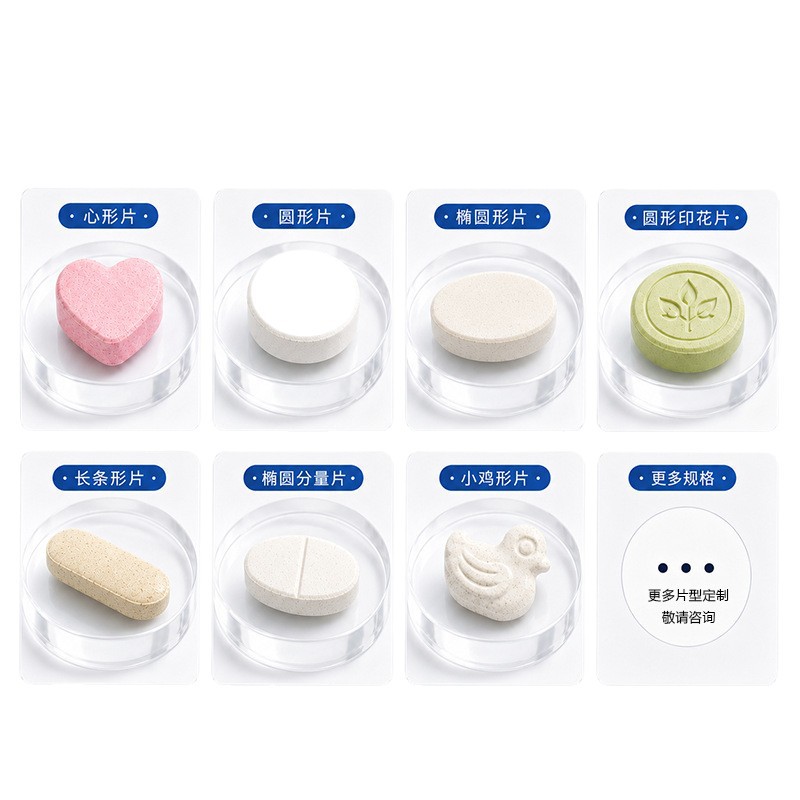
Why counting matters more for tablets
Counting error deserves more attention on tablets than on capsules or gummies for three reasons. First, scale: between a 60-count bottle and an 80-count bottle, three or four tablets either way is a small percentage, but it is immediately visible once the consumer opens the bottle. Second, cost structure: in a bottled product the tablets themselves are a large share of the total cost, so a persistent positive bias accumulates into real money over a year. Third, the regulatory lens: net content rules are written around weight or volume, and for counted products the actual count deviation usually surfaces before any weight deviation does. Together these mean counting accuracy drives both complaint rates and gross margin, so it cannot be treated as a small operational detail in the packing room.
Three counter principles and their weak points
Counting equipment falls into three families. Photoelectric counters register pulses as falling tablets interrupt a light path. They are simple and fast, but they over-count when tablets overlap or pass through together, and they are sensitive to dust. Vibratory tray counters with vision systems spread the tablets out and identify them one by one with a camera. Accuracy is high and oddly shaped tablets are handled well, at the cost of lower throughput and a strong dependence on stable lighting and background. Weight-based counters do not count at all; they infer the count from the average single-tablet weight. They are fast and indifferent to shape, but tablet weight variation translates directly into counting error, so they only suit products whose weight is already tightly controlled. Choose by first establishing how stable your weight and shape actually are, then balance speed against accuracy.
Material condition drives stability
The same counter performs differently across products mainly because of the material. Tablets with slightly high moisture become tacky and stick together, passing the light path as a single unit. Static makes light tablets cling to hopper walls or chutes, producing intermittent under-counts. On coated products, an over-thick film or excessive lubricant reduces shape consistency and makes the vision system's edge decisions harder. Broken and half tablets are another risk: left in the stream, they jam channels and cause runs of bad counts. The practical approach is to treat moisture, friability and visual acceptance rate as preconditions for the counting step. Get the tablets themselves stable before discussing equipment accuracy.
Matching the bottling line
Counting is one station on a line that also bottles, fills, adds desiccant, seals and labels. Those speeds have to match. If the counter outruns the sealer, tablets back up in the hopper and prolonged compression increases breakage; if the downstream is faster, bottles run empty and line efficiency drops anyway. Line selection also depends on how bottle mouth and tablet diameter fit together: a narrow mouth with large tablets bridges easily and needs vibration or air assistance to break the arch. Every change of bottle or tablet size requires re-calibration, and poor calibration shows up as erratic counts rather than a consistent bias in one direction.

In-line verification and rejection
Better-equipped lines verify the count a second time. One route is checkweighing after filling, using the difference between gross bottle weight and theoretical weight to flag an abnormal count. The other is vision inspection before capping, photographing the tablet layer and counting it directly. Both reject suspect bottles on the fly, but they see different things: weight catches systematic bias, vision catches local underfills. The rejection mechanism itself must be validated by seeding bottles with a known count and confirming both that the trigger fires and that the bottle lands in the right place. The value of verification is not perfect accuracy; it is catching deviations inside the factory instead of at the consumer's kitchen table.
Acceptance metrics and changeover
When accepting a counting and bottling system, look at five metrics at minimum: counting accuracy, stability over a run, rejection trigger rate, changeover time and breakage rate. Accuracy should be measured on samples drawn during continuous running rather than on a handful of bottles during commissioning. Stability is about the spread of deviation across a shift, not the average. Trigger rate needs seeded samples to confirm the verification step actually works. Changeover time is the key to flexible manufacturing: if switching moulds and settings takes more than half an hour, the cost of multi-product, small-batch orders rises sharply. Write these into the equipment acceptance sheet and the daily check sheet, and counting accuracy turns from an occasional complaint into a routine, managed figure.
Counting and bottling looks like an end-of-line detail, yet it moves complaint rates, packaging cost and line efficiency at the same time. Choose the right principle, keep tablet condition under control, match the line, then back it up with in-line verification and explicit acceptance metrics. That is the highest-return investment in pressed candy contract manufacturing. It is far cheaper to settle these points when selecting a line than to rework batch after batch once complaints arrive.
Related Products
Glycerol diester coffee OEM OEM OEM OEM OEM meal replacement coffee MCT live broadcast same solid beverage source manufacturer | GLP-1 Semaglutide Satiety & Fat Blocker Tablets | Custom Pressed Candy OEM Manufacturing
About Guangzhou Mesen Health Biotechnology Co., Ltd
Guangzhou Mesen Health Biotechnology Co., Ltd is located in the Huashan Science and Technology Park, Huadu District, Guangzhou. The company has focused on OEM and ODM services for the big health industry for nearly 20 years, operating dedicated research, production, sales and management centres, and maintaining long-term strategic partnerships with well-known Chinese medicine colleges and research institutions. Capabilities span pressed candy, gummies, capsules, solid beverages, herbal teas, plant beverages, protein powders, dietary supplements and enzyme jelly - from formulation development through contract manufacturing. For details on minimum order quantities, sampling lead times and quotations, see our manufacturing advantages and product range, or contact us for a tailored proposal.
Further Reading




