
Weighing and Bottle Filling Accuracy in Gummy OEM: Dosing and Checkweighing
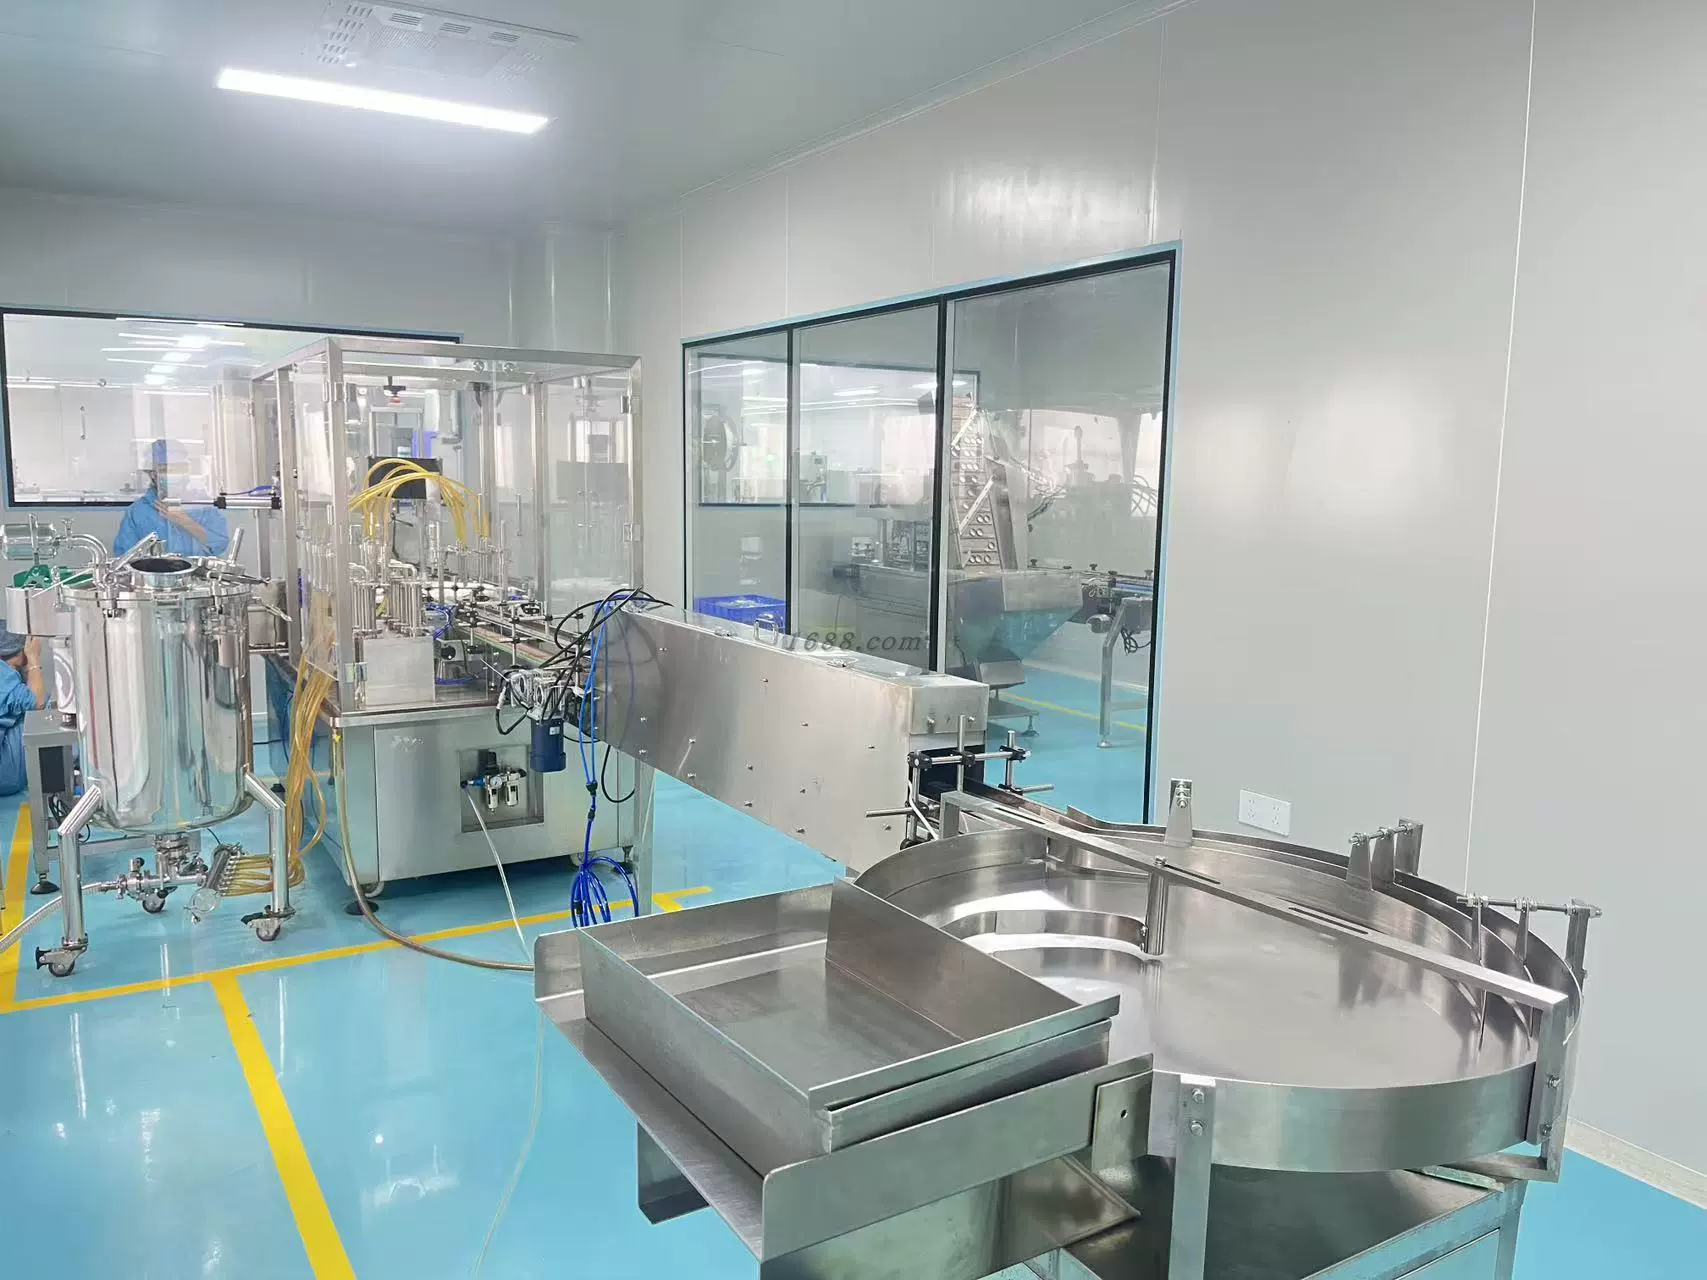
Gummies that look perfect coming off the front end often fail in the finished goods area, at weighing, dosing and bottle filling. Tablets can be counted by a counter, but gummies vary in shape, unit weight, surface friction and tackiness, so counting is unreliable and most lines switch to weight-based dosing. Weight dosing then has its own weaknesses: unit weight scatter, inconsistent feed and workshop humidity. The result is a batch where some bottles are light and others heavy, net content sits permanently on the negative tolerance limit, and one strict audit turns the whole lot into rework and sorting cost. This is how weighing and bottle filling accuracy is controlled in gummy contract manufacturing, from the choice of dosing principle to unit weight control upstream, sticky feed problems, checkweigher limits and filling verification.
Why finished dosing is harder for gummies than tablets
Tablet unit weight is usually held within a narrow range, so a counter using optical or mechanical detection can guarantee the count in each bottle. Gummies are different. Their unit weight has a genuinely wider distribution, because deposit volume, gel network strength, drying moisture loss and post-demoulding moisture regain all vary, and every one of them moves the weight of an individual piece. When unit weight scatter grows, counting cannot guarantee net content and weighing makes the piece count jump from bottle to bottle. Sticky surfaces make it worse: product hangs in the hopper and bridges in the chutes, and the faster the dosing cycle the more often it goes wrong. Finished dosing is therefore not one machine's job but a chain that runs from depositing and drying all the way to packaging.
Choose the dosing principle first
Selection depends on unit weight stability and on what the declared quantity actually is. Where unit weight is well controlled and the label promises a fixed number of pieces, counting is more direct, faster and yields tidier bottles, at the cost of any compensation for weight variation. Where unit weight varies or the label declares net content rather than piece count, weight dosing is steadier: it builds up to a target mass, so the piece count moves a little while net content stays under control. In practice many plants combine the two, filling close to target by weight and then verifying that the count falls inside a permitted band, leaving tolerance at both ends. The right question is never which machine is more advanced, but which of the two measures is the hard constraint.
Unit weight scatter is solved upstream
Nine out of ten weight problems in the finished goods area originate upstream. Narrowing unit weight starts at the depositor: whether every cavity dispenses the same volume, whether nozzles block or drip, and whether syrup temperature and viscosity hold steady. Drying comes next, because uneven temperature and humidity zones, airflow distribution or residence time leave tray edges and centres at different moisture levels, and they regain moisture differently after demoulding. Storage completes the picture, since gummies left too long in the pre-packing area keep gaining or losing moisture and become less stable the closer they get to the filler. Practical steps are to weigh samples by cavity and log the cavities that are outliers, to map actual temperature and humidity across the drying room, and to cap dwell time in the pre-packing area. Narrowing one point upstream often lifts filling yield far more than any change downstream.
Sticking, static and feed problems on the line
The most common failure in weight dosing is not inaccurate weighing but poor feed. Tacky surfaces bridge inside vibratory bowls and chutes, creating intermittent starvation. High humidity makes the product stickier, while low humidity builds static that pins pieces to the hopper wall. The usual answers are anti-stick surface treatment and regular cleaning of hoppers and chutes, holding the packing area within a stable temperature and humidity band rather than letting it swing, tuning drop height and vibration so pieces pass one at a time instead of chasing speed, and topping up the hopper in small, frequent charges so the product never compresses under its own weight. These adjustments look minor and in practice decide whether the filler can hold a stable pass rate.
Setting checkweigher limits
An in-line checkweigher is the last safeguard on filling accuracy. Set three limits: the target, the warning bands and the reject bands. Warnings flag a trend; rejects remove clearly non-conforming bottles; the gap between them absorbs the machine's own error. Limits cannot simply be copied from the declared net content, because the weight variation of bottle and cap has to be subtracted first, or good bottles will be rejected as waste. The checkweigher itself needs regular verification with certified weights, and the reject mechanism must be validated so that a bottle judged out of tolerance genuinely leaves the line and does not continue to case packing. On multi-SKU lines, limits must be re-set and a first-piece check performed after every format change, never carried over from the previous specification.
Filling verification and negative tolerance
Declared net content is a label promise and a favourite target of regulatory sampling, and it is judged on batch average and the range of negative deviation rather than on any single bottle. A verification routine therefore matters: draw bottles on a defined sampling plan, record average and range over time, and watch the trend. When readings drift consistently to one side, check the dosing setpoint first, then the material state, then the machine. Capping and sealing torque do not determine net content directly, but a failed seal lets moisture in and changes product weight, which distorts later verification data. Write the checkweigher limits, sampling frequency, verification records and non-conformance handling into a standard work instruction, so accuracy never depends on one experienced operator's feel.
Finished dosing accuracy in gummies is really a final audit of upstream process stability. Judging a contract manufacturer's filling capability needs no equipment list, only three questions: how unit weight is sampled and monitored, how weighing and counting are combined, and how checkweigher limits and verification frequency are set. A factory that answers those clearly will usually hold a stable fill rate.
Related Products
Greens Gummies with Multivitamin, Spirulina & Prebiotic Fiber | GREENS GUMMIES Supplement OEM | Feminine Balance Probiotic Gummies with Cranberry | Feminine Balance Gummies OEM
About Guangzhou Mesen Health Biotechnology Co., Ltd
Guangzhou Mesen Health Biotechnology Co., Ltd is located in the Huashan Science and Technology Park, Huadu District, Guangzhou. The company has focused on OEM and ODM services for the big health industry for nearly 20 years, operating dedicated research, production, sales and management centres, and maintaining long-term strategic partnerships with well-known Chinese medicine colleges and research institutions. Capabilities span pressed candy, gummies, capsules, solid beverages, herbal teas, plant beverages, protein powders, dietary supplements and enzyme jelly - from formulation development through contract manufacturing. For details on minimum order quantities, sampling lead times and quotations, see our manufacturing advantages and product range, or contact us for a tailored proposal.
Further Reading




